Setting up a controlled production space is easily one of the most critical and expensive investments an industrial facility will ever face. When your day-to-day operations have to fight off intense monsoon humidity, airborne dust, and strict international sterility audits, standard brick-and-mortar builders just don't have the technical chops to pull it off. For plant managers and project engineers actively searching for Clean Room Manufacturing Myanmar facilities can rely on, cutting corners is simply not an option. Costly delays with local supply chains, leaky wall joints, and HVAC setups that fail to keep up positive air pressure can easily derail your license before production even starts. That is why teaming up with a seasoned contractor for Clean Room Manufacturing Myanmar ensures your clean zones pass validation audits on the very first try. Investing in reliable Clean Room Manufacturing Myanmar shields your capital from expensive retrofits down the road, while relying on an established specialist in Clean Room Manufacturing Myanmar gives you the airtight panel systems, rock-solid humidity control, and energy savings your plant needs to operate around the clock.
Where Cleanroom Systems Deliver Real Production Impact
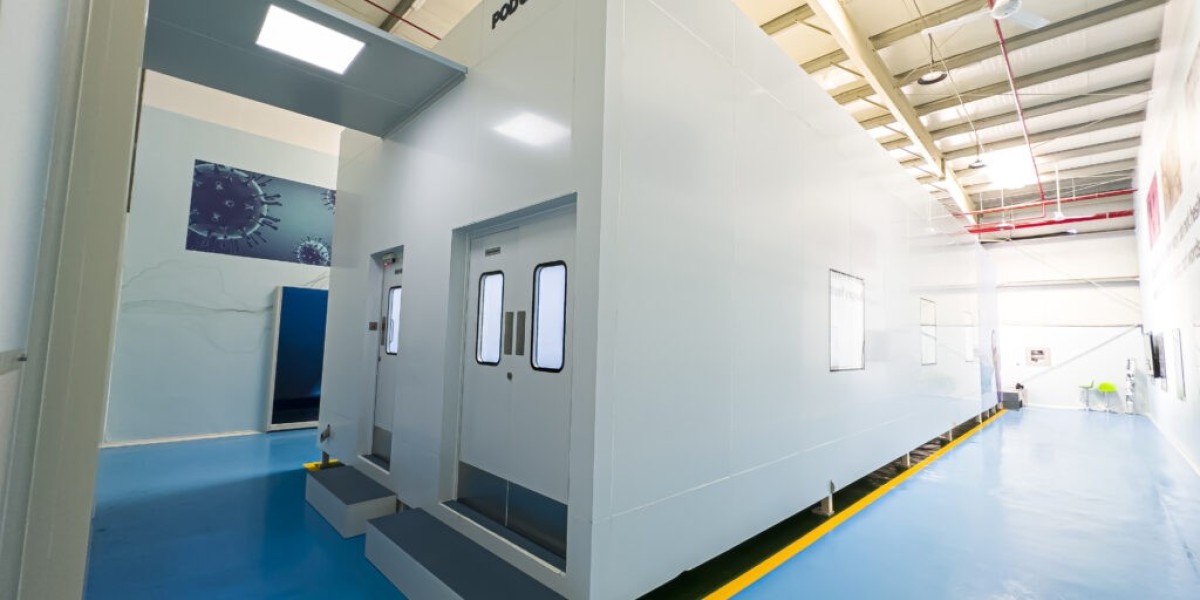
A cleanroom isn't just an insulated room with cold air running through it. It is a tightly balanced, precision-engineered enclosure built to keep out airborne dust particles, bleed off static charges, and prevent dangerous microbial growth across sensitive industrial sectors.
Pharmaceutical & Sterile Injectable Manufacturing
From established pharmaceutical manufacturing hubs in Yangon to new biotech labs, producing oral tablets, IV bags, and injectables means staying completely compliant with WHO-GMP and FDA benchmarks. A properly built clean suite maintains steady pressure cascades between rooms, stopping dust and bacteria from creeping from raw blending bays into sterile corridors and aseptic filling lines.
Precision Electronics, Optical Assembly & Testing
Inside high-tech industrial parks like Thilawa SEZ, microscopic dust specks can completely ruin printed circuit boards, sensors, and delicate lenses. When electronics engineers plan high-yield Clean Room Manufacturing Myanmar plants, they need continuous micro-particle protection across the floor. Choosing an advanced Clean Room Manufacturing Myanmar setup keeps static electricity from frying delicate semiconductors during delicate assembly stages. Rolling out a reliable Clean Room Manufacturing Myanmar layout prevents fine dust contamination across optical lens coating lines, while a certified Clean Room Manufacturing Myanmar facility ensures cleanroom bays maintain steady laminar airflow that safeguards sensitive high-tech yields.
Key Benefits of Working with a Specialised Cleanroom Builder
Skimping on cleanroom wall panels and air handling hardware just to shave a bit off initial construction costs always comes back to haunt you during audits. Choosing a specialized, dedicated modular builder brings concrete advantages to your plant's bottom line:
- Custom engineering built for tropical climates: Dedicated air handling units (AHUs) paired with industrial-grade dehumidifiers hold relative humidity steady, stopping moisture damage and mold dead in their tracks during heavy monsoon months.
- Airtight, non-shedding modular panels: Factory-made sandwich panels snap together with flush silicone coving and smooth anti-static finishes that hold up against harsh chemical washdowns year after year.
- Smart filtration that trims power bills: Premium HEPA and ULPA fan filter units provide smooth airflow velocities and required air change rates without running your electrical utility bill through the roof.
- Ironclad regulatory compliance: Every square meter is engineered from the ground up to satisfy ISO 14644-1 particle limits and EU-GMP Grade A through D cleanroom standards.
- Rapid modular installation: Prefabricated panels and ceilings assemble roughly 40% faster than traditional masonry construction, getting your facility up, validated, and profitable months ahead of schedule.
Our Streamlined 4-Step Cleanroom Delivery Process
Building a certified cleanroom shouldn't feel like wrestling with uncoordinated sub-contractors, mismatched panel shipments, and endless budget surprises. We follow an open, practical project workflow from day one through final testing:
Step 1: User Requirement Specification (URS) Analysis
Our cleanroom engineers sit down with your production team to review room classifications (from ISO Class 5 up to Class 8), pressure cascades, air change targets, and worker gowning flows to draw up an efficient layout.
Step 2: Customized Modular Engineering & Fabrication
We prepare a customized engineering blueprint featuring insulated PIR or rockwool panels, heavy-duty walk-on ceilings, motorized dynamic pass boxes, and interlocking personnel air showers tailored to your operations.
Step 3: Precision Installation & Clean Mechanical Integration
Our experienced field technicians erect the wall partitions, seal all light fixtures and utility penetrations with pharma-grade sealant, and integrate ducting so pressure cascades hold perfectly.
Step 4: Testing, Commissioning & DQ/IQ/OQ Handover
We run full on-site validation tests—including aerosol photometer HEPA leak testing (DOP/PAO), airborne particle counting, recovery rate checks, and airflow smoke patterns—handing over all signed qualification documentation.

Applications Across Specialized Facilities & Commercial Plants
Modern modular cleanroom architecture adapts just as easily to compact research labs as it does to sprawling industrial factories:
Healthcare Laboratories & Compounding Facilities
Hospital IVF units, diagnostic testing centers, and specialty compounding pharmacies need small, highly sanitary environments without dealing with heavy site dust. Pre-engineered modular pods drop right into existing warehouse or clinic spaces without disrupting day-to-day operations next door.
Large-Scale Commercial & High-End Industrial Plants
High-volume manufacturing plants require broad, unobstructed production floors with heavy utility integration. Choosing an experienced partner for Clean Room Manufacturing Myanmar manufacturers count on ensures heavy process equipment and overhead piping fit seamlessly. Implementing a Clean Room Manufacturing Myanmar design protects sensitive high-speed lines from ambient dust, while choosing a Clean Room Manufacturing Myanmar specialist allows facilities to expand modular production bays without tearing down existing infrastructure. Selecting an agile, high-end cleanroom setup guarantees your facility handles heavy output while staying fully compliant.
Why Leading Facility Managers Rely on Our Solutions
At the end of the day, picking a cleanroom partner comes down to proven mechanical engineering, durable structural materials, and technical crews who show up to help whenever you need them.
Our modular setups use non-shedding, corrosion-resistant panel skins and reliable air-handling equipment built to handle tough industrial plant environments. When operations directors scout for an established partner in Clean Room Manufacturing Myanmar markets respect, they look for turnkey accountability from architectural planning to final validation. That is why choosing our tested Clean Room Manufacturing Myanmar systems guarantees tight temperature and humidity control year-round. Investing in our verified Clean Room Manufacturing Myanmar infrastructure gives you durable facilities backed by experienced engineers, ensuring your manufacturing plant runs smoothly from day one.
Build Your Certified Cleanroom Facility Today
Do not let air leakage, high humidity, or failed validation inspections delay your commercial launch and regulatory approvals. Your operation needs a reliable controlled environment engineered for sterile safety, long-term durability, and complete peace of mind.
When you demand dependable quality, precision engineering, and turnkey expertise, choose the premier Cleanroom Manufacturer and solutions provided by Pod Tech Company. Contact our cleanroom engineering consultants today to discuss your URS, review floor plans, and receive a competitive proposal for your facility!
Frequently Asked Questions
1. How long does it usually take to install a modular cleanroom?
Depending on the overall square footage and target ISO classification, prefabricated modular cleanroom panels and ceilings can be installed and ready for testing within 6 to 12 weeks from finalized layout approval—far faster than brick-and-mortar builds.
2. How does the system handle high humidity during the Myanmar monsoon season?
Our air handling units come with dedicated desiccant wheels or deep-chilled water cooling coils engineered specifically for humid tropical climates. This keeps internal relative humidity locked between 45% and 55%, preventing condensation and mold.
3. What validation paperwork is included during the handover?
Every completed facility comes with a full documentation binder, including Design Qualification (DQ), Installation Qualification (IQ), and Operational Qualification (OQ) reports, along with certified HEPA filter leak test logs and particle count printouts.
4. Can these modular cleanroom walls be expanded or moved later?
Yes. Because the walls and ceilings use modular demountable panels rather than fixed masonry, you can easily shift wall lines, add new airlocks, or expand production bays with minimal site downtime as your output grows.
Thanks- mymesh.com for publishing this blog!