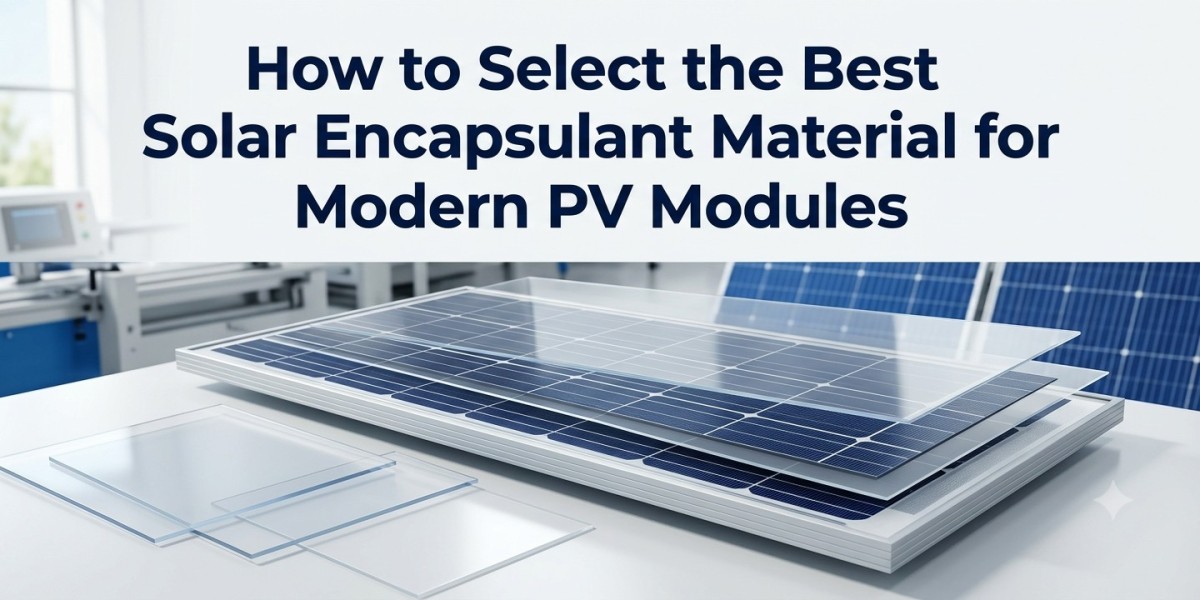
Solar panels really need dependable materials to keep, well, stable performance for many years. A key material is that encapsulant film; it kind of sits between the solar cells and the rest of the panel layers. It basically helps keep everything held together, protects the cells from moisture along with the usual environmental stress, and it also provides electrical insulation support.
Before these films end up in solar module production, manufacturers have to run quality checks with the right kinds of tests. Those checks help spot material defects early, keep production at the expected level, and lower the chance of panel failures later on. Sometimes it’s like you catch a small issue before it becomes a bigger one, you know, and everything stays stable, a bit more reliable.
For solar EPE encapsulant manufacturers, quality testing is pretty crucial, like even more than usual, since EPE is basically made from a blend of EVA and POE layers. Each layer sort of needs to do its own thing, with adhesion, optical clarity, and shielding in the mix, together. If one layer underperforms, the whole result can get weird, so testing becomes sort of unavoidable.
Why Quality Testing Is Important for Solar Encapsulant Films
Encapsulant films are, exposed to heat, sunlight, humidity, and other environmental conditions throughout a solar panel's service life, kind of, you know. If the material does n ot meet the required specifications, it can mess with adhesion, insulation, or even themodule'ss long-term reliability, and well, that turns into trouble later on.
Testing helps manufacturers kind of make sure the film lines up with the technical requirements for the solar module they plan to use. It also helps keep the output consistent across the production batches, and it cuts down on those lot-to-lot differences that are a bit annoying.
Reliable solar EPE film manufacturers usually do some set quality checks, like checking raw materials and finished films, plus how the film behaves while it’s being laminated. This kind of verification helps buyers pick the right solar film for their production style, not just go in with a blind leap and hope it works.
Key Quality Tests for Solar Encapsulant Films
Optical Transmittance Test
Optical transmittance is a measure of how much light actually goes through the encapsulant film — not more, not less. Since sunlight has to reach the solar cells, the film should let enough light through, but also avoid unwanted cloudiness or those visible defects you can sort of notice.
The manufacturers then check the film with optical measurement equipment that is actually meant for this kind of thing. Their results are later matched against the product specifications, plus the requirements that the solar module has to meet.
Good transparency helps with effective light transport in a practical way. For solar EPE encapsulant, this test matters a lot because the material needs proper optical characteristics and still keep the advantages that come from its layered architecture.
Peel Strength and Adhesion Test
Adhesion is another kinda important factor in solar panel quality, honestly. The encapsulant has to bond in a proper way with the glass, the solar cells, and also the other materials that are used in the module, even if that sounds obvious.
Peel strength testing measures the force needed to separate bonded layers under certain defined conditions. If adhesion is low, it may raise the risk of delamination, and that can let moisture get into the module; then it may start to affect performance later on.
Testing really should look at the relevant bonding surfaces and the lamination conditions, not just “the usual” routine. Solar EPE encapsulant manufacturers should check that the material meets the required adhesion specs before they approve it for regular production.
Gel Content Test
Gel content testing is commonly used for crosslinkable EVA-based encapsulants. It helps you see the level of polymer crosslinking after the material undergoes the required heating process, so you get a clearer idea of what happened.
Normally, the method goes by extracting the soluble bits from a cured specimen and then measuring what’s left as gel fraction. From that outcome, you can judge whether the encapsulant has reached the target degree of crosslinking, not just sort of, something approximate.
For EPE films, though, the test procedure has to fit the material’s exact makeup and structure. Because EPE has both EVA and POE, the testing has to use a validated method that matches the product, rather than leaning on assumptions from EVA alone, which can be a bit misleading.
Shrinkage Test
Encapsulant films may actually shrink when they are exposed to heat; sometimes it’s noticeable, sometimes it’s more subtle. If there is too much shrinkage during handling or lamination, it can lead to misalignment issues, those little wrinkles, or even a not-so-even coverage around the solar cells.
A shrinkage test is basically there to show how much the dimensions change under certain temperature and time settings. Usually t, the manufacturers line up the findings against the product’s approved boundaries, sort of like a pass/fail, but with limits instead.
When the shrinkage behavior stays stable and predictable, production teams can manage the film with less hassle and keep its placement accurate during module assembly. Buyers should not just look at the numbers; they should also verify the test conditions, because when comparing solarEPEe film products from different manufacturers, the reported results can look similar,r but the context—well, that context can be different.
Thermal Stability Test
Solar encapsulant films have to tolerate the heat that is used during lamination and also all the temperature changes you get during service. Thermal testing helps to judge how the material sort of responds to certain heating conditions that are defined.
Depending on the product and where it’s going to be used, manufacturers might check dimensional stability, any shift in the look of the film, and other useful properties after heat exposure, too.
These outcomes allow the team to see whether the film works for the planned manufacturing process. SolarEPEe encapsulant should be tested under conditions that match its technical specifications and the actual use it’s meant for, not just generic settings.
Moisture Resistance Test
Moisture can kind of mess with solar module materials, and it may contribute to corrosion, loss of adhesion, or electrical performance hiccups. So the encapsulant films need an appropriate level of resistance to moisture under the conditions that are expected during service life, you know.
Testing might involve measuring water absorption, or doing water vapour transmission tests, depending on the material and what it is meant to do. Those approaches don’t check exactly the same things, so the chosen test should align with the quality requirement that is actually being checked.
For solar EPE encapsulant manufacturers, moisture-based testing matters; it helps confirm whether the film actually meets the requirements for the target module design and the operating environment.
Electrical Insulation Test
Electrical insulation helps protect the solar module from unwanted current leakage. The encapsulant films should give the right electrical properties for the module design and the operating voltage, too, in a way that makes sense during use.
Testing might include volume resistivity, dielectric strength, or maybe other electrical measures that are set for the material. In other words, each little test checks a separate aspect of electrical performance, sort of how it behaves under different conditions.
Manufacturers should really use well-known test methods, and then compare those results with the relevant technical requirements, as it matters. These checks are particularly important for modules intended for demanding operating conditions.
UV and Weather Resistance Test
Solar panels stay outside for long stretches, so the stuff they’re made from has to take sunlight and all kinds of shifting weather, like, you know, rain, wind, temperature swings. The UV part can make certain polymers change tone, sort of dull, or gradually lose useful properties, even if that happens slowly.
In accelerated weathering tests, the samples get exposed to carefully controlled UV radiation and heat and, when needed, moisture too. After that, the pieces are looked at again for any changes in look and in a few chosen performance properties.
These tests help manufacturers figure out how the material reacts to simulated environmental strain. They still don’t really give a precise estimate of the module service life, but they do help with material comparison and general quality checks, kind of more grounded.
How Manufacturers Should Maintain Quality Control
Testing each individual property i s useful, but honestly a full quality process needs more than just measurements; it also needs consistent documentation and some real production controls, even if it sounds a bit redundant.
Good solar EPE film manufacturers should keep batch identification, the test reports, material specifications, and a record of the production conditions. Incoming raw materials should be reviewed, and then finished films should be checked for thickness variation, contamination, bubbles, and a bunch of other obvious defects you can usually spot.
Sample testing should follow written procedures and use calibrated equipment, plus clear acceptance limits that are not “kinda ok” but actually stated. The manufacturer should also look at customer feedback, then investigate recurring defects so the real origin can be found, not just treated.
Before buyers pick a supplier, they should ask for the latest technical data sheets and any relevant test reports. It also helps to verify which methods were applied, what conditions were used during testing, a nd whether the results fit the requirements of the intended module.
Final Thoughts
Quality testing helps ensure that solar encapsulant films kinda meet the needs of modern solar module production. Optical transmittance, adhesion, gel content, shrinkage, thermal stability, moisture resistance, electrical insulation, and weather resistance are all important areas to check. Not just one item either; you really want the whole set.
For buyers comparing solar EPE encapsulant manufacturers, the best approach is to review product specs, any relevant test reports, and batch consistency instead of just going by price alone. Otherwise, you end up comparing the wrong things, even if the numbers look fine.
A reliable solar EPE encapsulant should satisfy the requirements of the intended module design and manufacturing process. Careful testing, plus clear quality records, helps manufacturers reduce production issues and build solar panels with dependable performance. In the end, it’s less guesswork and more repeatability.