Industrial Machine Vision enables manufacturers to collect visual data that can support automated decision-making and production control. Processed images can provide information about product quality, position, dimensions, or identification characteristics. This creates opportunities for greater integration between inspection and industrial automation systems.
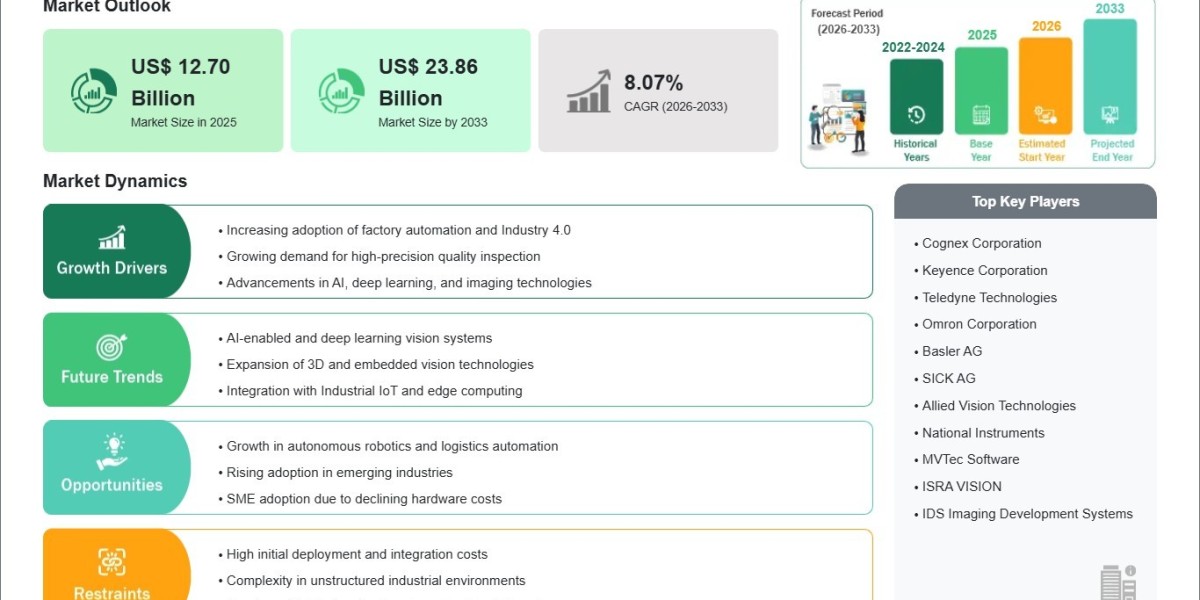
The Industrial Machine Vision market Share is expected to reach US$ 23.86 billion by 2033 from US$ 12.70 billion in 2025. The market is estimated to record a CAGR of 8.07% from 2026 to 2033. The increasing adoption of automation, demand for consistent product quality, and growing need for efficient production processes are supporting the use of machine vision technologies across industrial operations. Manufacturers are increasingly integrating vision-based systems into production environments to automate inspection activities, identify defects, improve process accuracy, and support faster decision-making.
Industrial machine vision systems play an important role in modern manufacturing by enabling machines to interpret visual information and perform inspection or identification tasks with limited manual intervention. These systems can be integrated into production lines to examine products, components, packaging, and materials at different stages of manufacturing. By continuously analyzing visual information, machine vision can help manufacturers maintain consistent production standards while supporting automated quality-control processes.
Quality inspection represents a major application area for industrial machine vision. Manufacturers can use cameras and imaging systems to detect surface defects, dimensional variations, incorrect assembly, missing components, and other quality-related issues. Automated inspection can provide consistent evaluation across large production volumes and help identify problems earlier in the manufacturing process.
Download Sample PDF Now: https://www.businessmarketinsights.com/sample/BMIPUB00035116
Industrial machine vision is also being integrated into automated production and assembly operations. Vision systems can assist robots and other automated equipment by providing information about the position, orientation, shape, or appearance of components. This enables automated systems to perform tasks such as part handling, assembly, sorting, and positioning with greater precision and repeatability.
The technology is gaining importance across industries where accuracy, speed, and product consistency are essential. Automotive manufacturing, electronics, pharmaceuticals, food and beverages, packaging, consumer goods, and other industrial sectors can use machine vision for inspection, identification, measurement, and process monitoring. The flexibility of vision-based technologies allows manufacturers to adapt these systems to different production requirements and operating environments.
Advancements in imaging technologies, sensors, cameras, artificial intelligence, and image-processing software are further improving machine vision capabilities. Modern systems can process visual information more efficiently and support increasingly sophisticated inspection requirements. Integration with industrial automation platforms can also enable machine vision systems to communicate with production equipment and contribute to more connected manufacturing processes.
The growing focus on smart manufacturing is creating additional opportunities for machine vision adoption. Connected production environments increasingly depend on automated systems that can collect information, identify process variations, and support operational decisions. Machine vision can contribute to these environments by providing visual data that can be used alongside other industrial information to improve visibility across production processes.
Machine vision also supports traceability and identification applications. Vision systems can read codes, labels, markings, and other visual identifiers to help manufacturers track products and components throughout production and packaging operations. Automated identification can support organized workflows while reducing the dependence on manual verification.
Explore our Industry Snapshots — a visual look at the latest trends, insights and developments shaping the industry.: https://www.businessmarketinsights.com/industry-overview/industrial-machine-vision-market
The increasing emphasis on production efficiency and reliable quality control is expected to encourage continued investment in industrial machine vision solutions. Manufacturers are seeking technologies that can support automated inspection, reduce process inconsistencies, improve operational visibility, and integrate effectively with existing production systems. These requirements are contributing to broader adoption of vision technologies across diverse industrial applications.
Future opportunities for industrial machine vision are closely associated with advances in automation, intelligent image analysis, connected manufacturing, and robotics. As industrial environments become increasingly automated, the ability to capture and interpret visual information can become an important part of production management. Continued development of machine vision technologies can support manufacturers in improving inspection processes, enhancing automation capabilities, and building more efficient and responsive industrial operations.
FAQ's
1. What is industrial machine vision used for?
Industrial machine vision is used for automated inspection, quality control, measurement, identification, sorting, assembly assistance, and process monitoring. It enables industrial systems to analyze visual information and support manufacturing tasks with greater consistency and automation.
2. What factors are supporting the growth of industrial machine vision?
Key factors include increasing industrial automation, demand for consistent product quality, adoption of smart manufacturing, growing use of robotics, the need for automated inspection, and advancements in cameras, sensors, image processing, and intelligent vision technologies.
Discover More Research Reports by Business Market Insights:
3D Gaming Console Market Trends, Demand & Growth by 2033
8K Technology Market Growth, Size & Forecast by 2033
High Definition (HD) Voice Market Share, Growth & Demand by 2033
Motor Control Centers Market Growth, Trends & Demand by 2033