
Introduction
A reliable Shell and Tube Heat Exchanger Supplier does more than provide equipment. In petrochemical plants, supplier expertise can influence thermal performance, maintenance planning, operational safety and the ability to keep production running consistently.
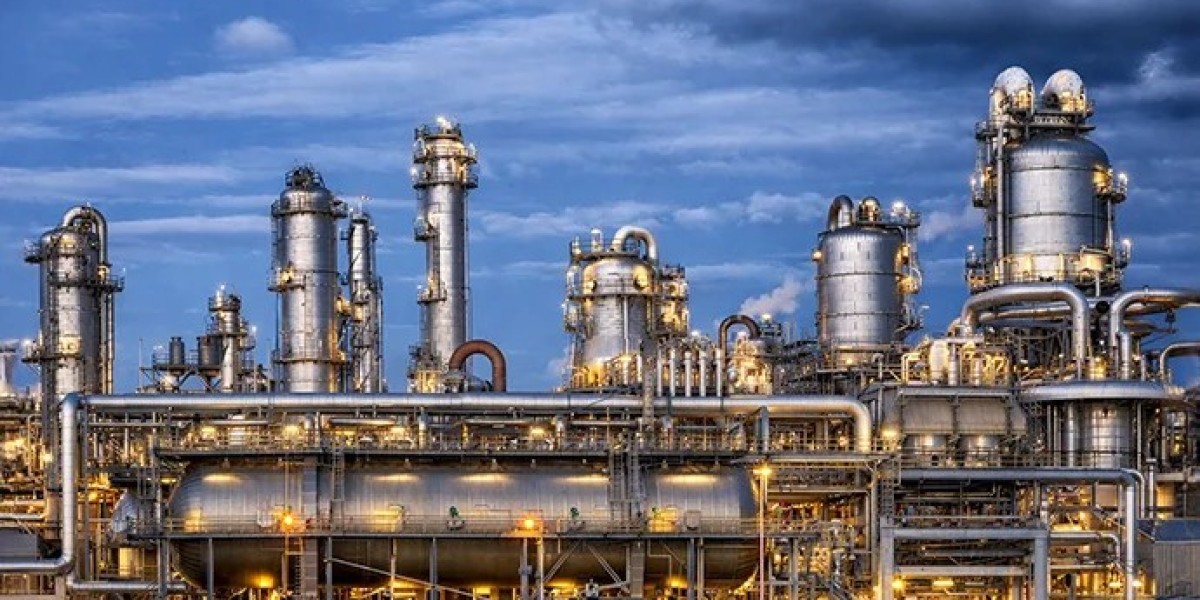
Petrochemical processes often involve high temperatures, pressures, corrosive fluids and demanding heat duties. Even a relatively small loss in heat transfer performance can affect product quality, energy consumption and overall plant productivity.
This is why selecting the right supplier should be considered an engineering decision as well as a procurement decision. The right technical knowledge can help ensure that a heat exchanger is suited to the process rather than simply meeting a basic specification.
Why Continuous Production Depends on Heat Transfer
Heat exchangers are involved in many petrochemical operations, including heating, cooling, condensation and heat recovery. Their performance directly affects how efficiently heat moves between process streams.
When an exchanger becomes fouled, develops a leak or experiences excessive pressure drop, the consequences can extend beyond the equipment itself. Operators may need to reduce throughput, increase utility consumption or schedule an unplanned shutdown.
An experienced Shell and Tube Heat Exchanger Supplier understands these operating challenges and can consider them during equipment selection and design.
Where Supplier Expertise Makes a Difference
1. Understanding the Process Conditions
A good design begins with an accurate understanding of the application. Fluid properties, flow rates, operating temperatures, pressures, allowable pressure drop and fouling tendencies all influence exchanger performance.
Supplier engineering expertise helps translate these process requirements into practical design decisions. This can include selecting suitable tube dimensions, materials, flow arrangements and heat transfer surfaces.
2. Managing Fouling and Maintenance
Fouling is a common challenge in petrochemical processing. Deposits on heat transfer surfaces reduce thermal efficiency and can increase pressure drop.
A knowledgeable Shell and Tube Heat Exchanger Supplier can consider fouling tendencies while developing the design, including appropriate flow velocities, tube layouts and cleaning provisions.
Designing with maintenance in mind can make inspection and cleaning more manageable, helping operators maintain performance throughout the equipment's service life.
3. Selecting Materials for Difficult Environments
Petrochemical fluids can create demanding corrosion conditions. Choosing materials solely on initial cost may increase the risk of premature deterioration.
Supplier expertise helps evaluate material compatibility with process fluids, temperatures and pressures. The objective is to achieve a sensible balance between corrosion resistance, mechanical integrity, thermal performance and lifecycle cost.
Key areas where supplier expertise supports reliability
Thermal design: Helps achieve the required heat duty without unnecessary oversizing.
Material selection: Supports resistance to corrosion and process-related degradation.
Mechanical design: Addresses pressure, temperature and thermal stresses.
Cleanability: Makes routine maintenance more practical.
Inspection access: Supports easier monitoring of equipment condition.
Performance margins: Provides appropriate allowance for realistic operating conditions.
Supporting Stable Petrochemical Operations
Continuous production does not mean operating equipment without interruption or maintenance. It means creating a system where equipment performance remains predictable and maintenance can be planned rather than forced by unexpected failures.
A capable Shell and Tube Heat Exchanger Supplier can contribute to this approach by considering the complete operating lifecycle. Design reviews, fabrication quality, inspection requirements and testing all have a role to play.
Quality control is particularly important for industrial heat exchangers because manufacturing defects or dimensional inconsistencies can affect performance and reliability. Appropriate inspection and testing provide greater confidence before equipment enters service.
Energy Efficiency and Sustainability
Heat exchanger performance also has an environmental dimension. Poor heat transfer can increase the amount of steam, cooling water, electricity or fuel required to achieve the same process result.
For petrochemical facilities seeking to reduce energy consumption and emissions, well-designed heat recovery systems can provide an important opportunity. A knowledgeable Shell and Tube Heat Exchanger Supplier can help evaluate where process heat can be recovered and reused effectively.
Better thermal performance can therefore support both operational efficiency and broader sustainability objectives.
Choosing a Supplier for Long-Term Value
The lowest purchase price does not necessarily represent the lowest overall cost. An exchanger that requires frequent cleaning, loses performance quickly or causes production interruptions may become considerably more expensive over its operating life.
When evaluating a Shell and Tube Heat Exchanger Supplier, buyers should consider:
Engineering capability and application experience
Understanding of petrochemical process conditions
Material and fabrication expertise
Quality assurance and inspection practices
Maintenance and cleanability considerations
Ability to accommodate customised requirements
Technical documentation and testing
Long-term service and replacement support
These factors provide a more realistic picture of the supplier's ability to contribute to plant reliability.
Conclusion
Continuous petrochemical production depends on thousands of interconnected decisions, and heat exchanger performance is one of them. Choosing an experienced Shell and Tube Heat Exchanger Supplier can help plants address thermal performance, fouling, materials, maintenance and lifecycle reliability from the design stage onwards.
Precision Equipments has been a leading manufacturer and supplier of Shell and Tube Heat Exchangers and process equipment since 1981, serving key sectors such as Oil & Gas, Petrochemicals, Fertilizers, Power Plants, LNG and Nuclear Energy. Its long-standing industry presence reflects the importance of combining sound engineering with dependable equipment for demanding process applications.
Ultimately, effective heat exchanger selection is not simply about transferring heat. It is about supporting safer, more efficient and more predictable production over the long term.
Frequently Asked Questions(FAQs)
What should petrochemical plants look for in a Shell and Tube Heat Exchanger Supplier?
They should consider engineering expertise, material selection, thermal and mechanical design capabilities, quality control, maintainability, testing and lifecycle support.
How can a heat exchanger supplier help reduce petrochemical downtime?
A supplier can support reliability through appropriate design, material selection, fouling considerations, inspection provisions and maintainability features that reduce the likelihood and impact of unexpected failures.
Why is material selection important for petrochemical heat exchangers?
Petrochemical streams can be corrosive and may operate at high temperatures and pressures. Appropriate materials help maintain mechanical integrity and extend equipment service life.
Can heat exchanger supplier expertise improve energy efficiency?
Yes. Correct thermal design can improve heat recovery, reduce unnecessary utility consumption and help maintain heat transfer performance during operation.