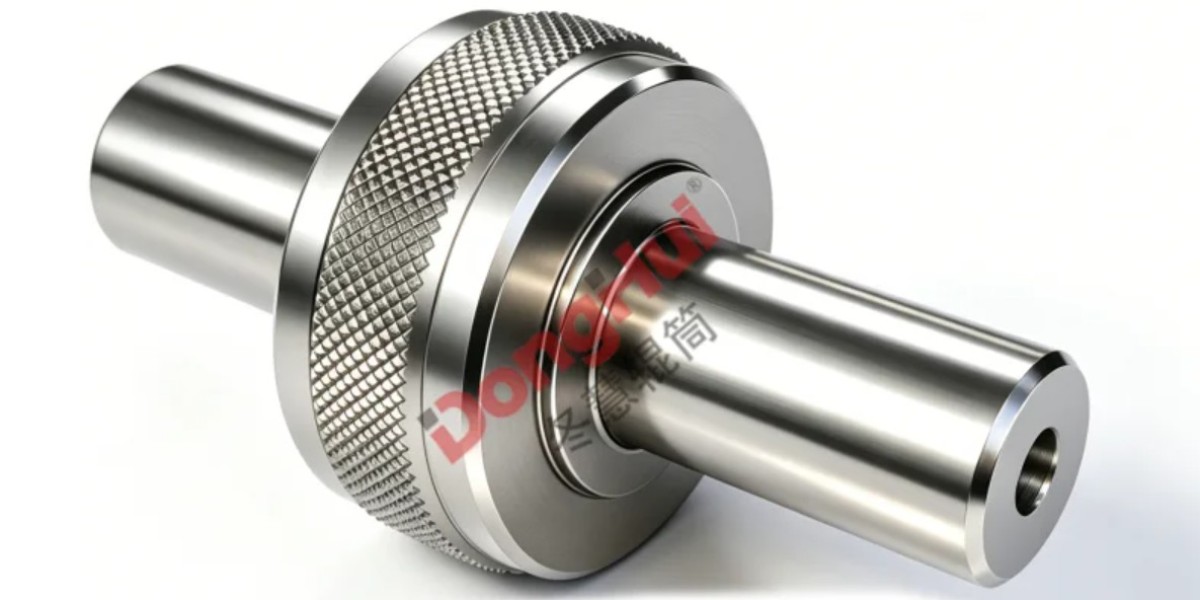
Precision Grid Knurling is the main component of the quantitative ink supply system in flexographic printing machines. Besides, it is also regarded as the heart of the flexographic printing machine. The quality of Precision Grid Knurling directly affects the quality and effect of the printed products.
The ink transfer performance of Precision Grid Knurling refers to its ability and uniformity to receive and transfer ink. The ink transfer performance of Precision Grid Knurling is related to the shape of the mesh holes, the angle of arrangement, the capacity, as well as the number of lines and the materials used in the production of Precision Grid Knurling. The following will discuss the influence of these factors on the ink transfer performance of Precision Grid Knurling.
1. Mesh Hole Shape and Arrangement Angle
The opening shape of the mesh holes when viewed from above includes rhombic and regular hexagonal shapes. The opening of the regular hexagonal mesh holes is larger, thus having better ink receiving and transfer performance than the rhombic ones. The cross-sectional shape of the mesh holes is generally spherical, which makes the mesh wall smooth and conducive to ink transfer. The arrangement angle of the mesh holes is generally 30°, 45°, and 60°.
The 30° regular hexagonal mesh holes have better ink release and transfer performance, but the mesh wall on the surface of Precision Grid Knurling causes excessive wear between the ink knife and Precision Grid Knurling, and the mesh wall will disrupt the uniformity of ink flow. Therefore, 30° regular hexagonal mesh holes are difficult to produce a uniform ink film.
The 45° rhombic mesh holes have better working performance, but their mesh wall is generally 15-20 μm wide, resulting in a larger mesh gap and less uniform ink transfer. Moreover, the communication pipeline shape of the 45° rhombic mesh holes has a tendency to be too deep, which will reduce ink release, facilitate ink transfer, increase ink blockage at the bottom of the ink injection holes, and increase the difficulty of cleaning.
For 60° regular hexagonal mesh holes, due to their effective geometric shape, they can maximize the utilization of space, and the 60° arrangement method makes the mesh holes compact, that is, on the same area of Precision Grid Knurling surface, more mesh holes of the same size can be engraved, transferring more ink. Through mathematical calculation, it can be known that in the same area range, the space area occupied by the 60° regular hexagonal mesh holes is 15% more than that of the rhombic mesh holes, which means that the 60° regular hexagonal mesh holes can be engraved shallower without affecting the original capacity. Therefore, when transferring the same ink volume, the 60° regular hexagonal mesh holes can be engraved more shallowly, which is conducive to ink transfer.
The precision grid knurling with 45° and 30° arrangements is now generally only used for coating, laminating, and some special printing aspects. Ordinary flexographic printing does not use it anymore. The most widely used precision grid knurling with 60° arrangement is the one used in production.
2. Mesh Hole Capacity
Mesh hole capacity refers to the amount of ink that Precision Grid Knurling can accommodate per unit area under normal conditions. The unit is BCMin21010 μm3/in2. The capacity of the mesh hole is related to the depth and opening degree of the mesh hole. When the volume of the mesh hole is constant, the depth of the mesh hole is inversely proportional to the opening degree. Generally, the depth of the mesh hole is 23% to 33% of the opening (that is, if the opening of the mesh hole is 100 μm, then its depth is 23-33 μm, which is ideal at 28%).
The size of the mesh capacity has a significant impact on the enlargement of the dots in printing. A larger mesh capacity means a greater amount of ink is transferred, making the dots more likely to enlarge; while a smaller mesh capacity results in only a small amount of ink being transferred to the substrate during the printing process, which is beneficial for preventing dot enlargement and ink flying, and ensuring the quality of printing. Therefore, the mesh capacity should be as small as possible while meeting the ink transfer requirements. This also confirms that the 60° arranged regular hexagonal precision grid knurling is the best. This arrangement enables more equal volume mesh holes to be arranged on a unit area, and when the same amount of ink is transferred, the mesh holes can be made smaller.
III. The number of lines in precision grid knurling
The number of lines in precision grid knurling refers to the number of mesh holes per unit length along the axial direction of precision grid knurling, which determines the uniformity and ink transfer volume of precision grid knurling. The higher the number of lines in precision grid knurling, the closer the ink layer on precision grid knurling is to a "continuous" state. Additionally, the number of lines in precision grid knurling has a direct relationship with its capacity, so it has a significant impact on the ink transfer volume. When the number of lines in precision grid knurling increases, the opening area of the ink holes decreases, the capacity becomes smaller, and thus the ink transfer volume also decreases. Therefore, the higher the number of lines in precision grid knurling, the smaller the ink transfer volume.
The number of lines in precision grid knurling determines its applicable range. Generally, when printing large-area solid color blocks or images with less demanding requirements, a low-numbered precision grid knurling is considered: while for halftone or black printing, a high-numbered precision grid knurling is required to ensure that the opening area of the ink holes is smaller than the smallest dot area on the plate, thereby reducing dot enlargement. The mesh line number of precision grid knurling must match the printing mesh line number, with a ratio of approximately 51 for individual fine products, and this ratio may be higher for specific products. However, the number of lines in precision grid knurling is not always higher is better. A very high number of lines makes it difficult for the ink holes to release ink after ink application, resulting in insufficient ink supply and insufficient solid density, causing ink bleeding. Therefore, the selection of precision grid knurling should not only focus on the high number of lines in precision grid knurling, but also consider the printing density. In practical work, the number of lines must be reasonably selected based on different grades of printed products.
precision grid knurling https://www.rollerchina.com/knurling-cutter-g-grid.html